Coal-Fired Thermal Power Plant
Process Overview
Coal-Fired Thermal Power Plant — Process Overview
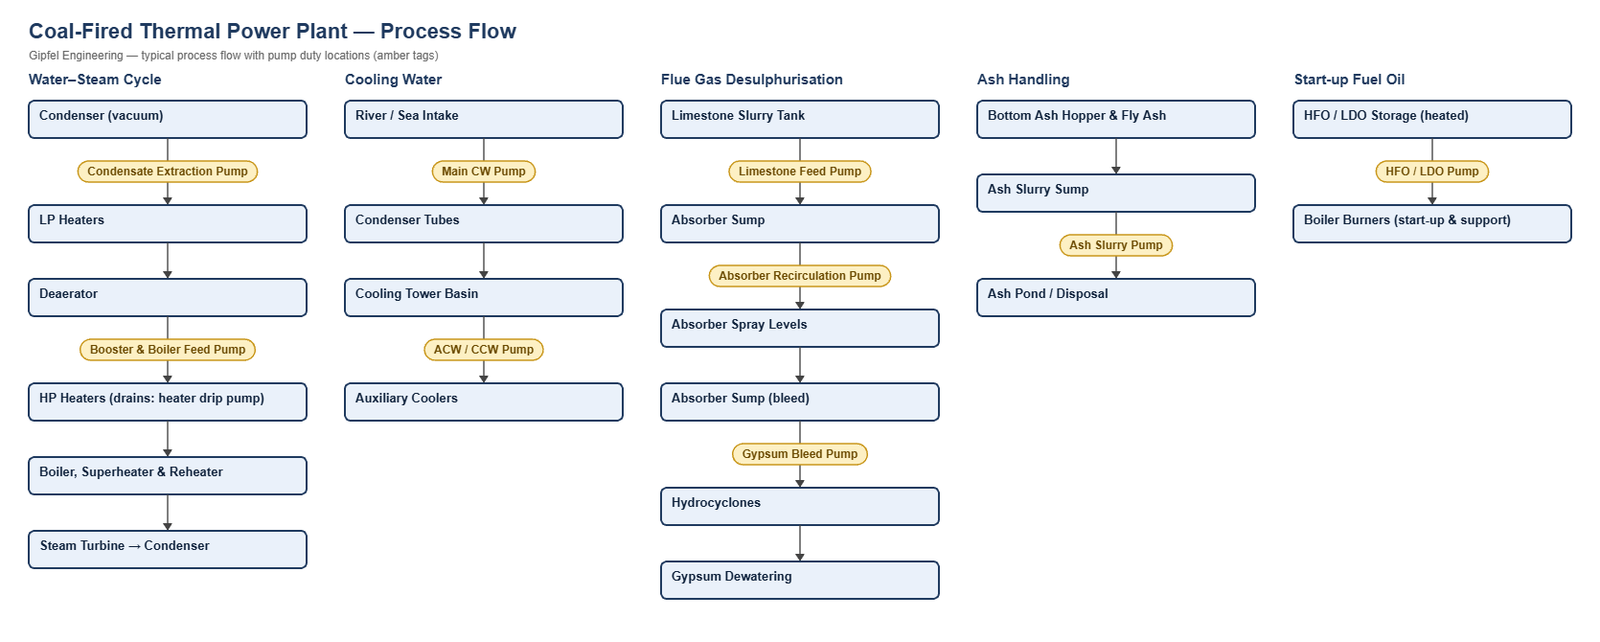
In a coal-fired (Rankine-cycle) station, demineralised feedwater is pumped to boiler pressure, converted to superheated steam, expanded through the turbine and condensed under vacuum before returning through the heaters to the deaerator. Auxiliary circuits handle cooling water, flue gas desulphurisation (FGD) slurry, ash disposal and start-up fuel oil. Each circuit sets a different sealing problem: low-lubricity hot water close to saturation, vacuum suction, abrasive slurry and heavy oil.
This page covers subcritical and supercritical pulverised-coal units. For bagasse and biomass boilers see Co-Generation & Biomass; for gas-turbine plants with heat recovery steam generators see Combined Cycle (CCGT).
Key Sealing Challenges
- Boiler feed pumps: feedwater at 145–185 °C close to its saturation temperature. The seal is sized for seal-chamber pressure and cooled with API Plan 23.
- Condensate extraction pumps: suction under vacuum, so air must not be drawn across the seal faces into the condenser.
- FGD and ash slurry: abrasive solids need hard-face pairs, external-spring designs and a clean flush or pressurised barrier.
- Heavy fuel oil: coking on the atmospheric side is controlled with an API Plan 62 steam quench.
What mechanical seal is used in power plant boiler feed pumps (BFP)?
Boiler feed pumps typically use balanced cartridge mechanical seals with stationary springs (e.g. Gipfel HP760) on an API Plan 23 cooling circuit. Feedwater at 145–185 °C has little lubricity and flashes easily, so a pumping ring circulates seal-chamber water through a cooler to keep it below the seal’s temperature limit. Silicon carbide vs. carbon faces are common. The seal is sized for seal-chamber pressure (close to suction or balance-line pressure), not pump discharge.
Root-Cause Failure Analysis — Field Example
Symptom: Boiler Feed Pump (BFP) seal shows intermittent carbon face blistering and popping sound during unit load changes.
  ├── Incorrect Response: "Install harder tungsten carbide faces."
  ├── Diagnostic Evidence Required:
  │     ├── Inspect carbon face under 50x magnification: look for crater-like pits (vapour trapped in carbon pores).
  │     ├── Review API Plan 23 cooler delta-T: is the cooler fouled or air-bound, letting seal-chamber temperature rise above the seal datasheet limit?
  │     └── Check deaerator pressure during turbine trip: did suction pressure fall towards vapour pressure?
  └── Engineered Solution:
        ├── Fine-grain, low-porosity electro-graphite carbon paired with reaction-bonded SiC.
        ├── Clean, vent and re-rate the Plan 23 loop; keep cooler outlet within the seal datasheet limit.
        └── Maintain the NPSH margin (NPSHa − NPSHr) recommended by the pump OEM during load transients.
Operational & Environmental Benefits
- Lower heat loss with API Plan 23 vs. Plan 21: Plan 21 continuously cools a stream taken from pump discharge; Plan 23 cools only the small closed volume in the seal chamber. It removes far less heat from the feedwater cycle and needs a smaller cooler, which is why API 682 identifies Plan 23 as the preferred plan for hot-water services. Calculate site savings from the actual cooler duty.
- Reduced demineralised-water loss: replacing packed glands on hot-water auxiliaries with mechanical seals cuts continuous leakage of treated water. Quantify only from site measurements.
Frequently Asked Questions
Why is API Plan 23 preferred over API Plan 21 for boiler feed pumps?
Plan 23 recirculates only the water inside the seal chamber through a cooler using an integral pumping ring, while Plan 21 cools a continuous flow of hot discharge feedwater. Plan 23 therefore needs less cooling water and removes less heat from the cycle while keeping the seal faces below their vaporisation limit.
How is air ingress prevented in condensate extraction pumps (CEP)?
Where the seal chamber is under vacuum, a balanced cartridge seal is supplied with an API Plan 32 condensate injection to hold the chamber above atmospheric pressure, with a Plan 62 quench on the atmospheric side. Where air ingress is critical, a pressurised double seal with a Plan 53A barrier is used.
Which seal faces suit FGD limestone and gypsum slurry?
Sintered silicon carbide against sintered silicon carbide in a slurry cartridge with external springs, so the springs stay out of the slurry. Single seals use a Plan 32 clean water flush where dilution is acceptable; otherwise a pressurised double seal with a Plan 53A barrier at least 1.4 bar above seal-chamber pressure.
Related: Co-Generation & Biomass · Combined Cycle (CCGT) · Mining Slurry.
Request a Seal Selection
Send your pump make and model, fluid, temperature, pressure, shaft size and speed to info@gipfelengg.com or use our enquiry form. Gipfel Engineering (ISO 9001:2015, NSIC-registered MSME, Mumbai) designs and manufactures mechanical seals, seal support systems and process pumps.
Equipment solutions: Boiler Feed & Multistage Pumps · Vertical & Sump Pumps · Slurry Pumps · Turbines.
Pump Duty & Mechanical Seal Selection Matrix
Typical values for selection guidance only. Final selection is made against the customer duty sheet.
| Pump duty | Fluid | Typical temp. | Typical pressure (bar) | Seal arrangement | Faces / elastomer | API piping plan |
|---|---|---|---|---|---|---|
| Boiler Feed Pump (BFP), motor- or turbine-driven | Demineralised feedwater (AVT / OT treated) | 145–185 °C | Discharge about 170 bar (subcritical) to over 300 bar (supercritical). The seal sees seal-chamber (suction / balance-line) pressure, not discharge — confirm per pump | High-pressure balanced cartridge, stationary springs (catalogue ref. HP760) | Reaction-bonded SiC vs electro-graphite carbon / EPDM (peroxide-cured) or FEPM (Aflas) | API Plan 23 (pumping ring + seal cooler) |
| BFP Booster Pump | Deaerated feedwater | 140–170 °C | Suction = deaerator pressure plus static head — confirm per pump | Balanced multi-spring cartridge | SiC vs antimony-impregnated carbon / EPDM (peroxide-cured) or FEPM | API Plan 23 |
| Condensate Extraction Pump (CEP) | Turbine condensate | 35–55 °C | Suction under condenser vacuum. Seal chamber may be under vacuum or at reduced pressure, depending on throttle-bush / balance-line design — confirm per pump | Balanced multi-spring cartridge; Double cartridge, back-to-back (pressurised) where air ingress is critical | SiC vs carbon / EPDM | API Plan 32 (condensate injection) + Plan 62 quench, or dual seal with Plan 53A |
| Heater Drip / Drain Pump | Saturated heater drains | 120–180 °C | Suction close to saturation; low NPSH margin | Balanced multi-spring cartridge | SiC vs carbon / EPDM (peroxide-cured) or FEPM | API Plan 23 |
| Main Cooling Water (CW) Pump | Raw river, lake or sea water | 25–40 °C | 2–4 bar | Balanced multi-spring cartridge | SiC vs SiC / EPDM or FKM | API Plan 32 (filtered clean water) for silt-laden water; Plan 11 only for clarified water |
| Auxiliary / Closed Cooling Water Pump (ACW / CCW) | Treated cooling water or inhibited DM water | 30–45 °C | 3–8 bar | Wave-spring semi-cartridge | SiC vs carbon / EPDM | API Plan 11 |
| DM Water Transfer / Make-up Pump | Demineralised water | Ambient | 3–8 bar | Single-spring seal | SiC vs carbon / EPDM | API Plan 11 |
| Boiler Blowdown / Drain Flash Pump | Hot blowdown water | 100–140 °C | 2–6 bar | Balanced multi-spring cartridge | SiC vs carbon / EPDM (peroxide-cured) or FEPM | API Plan 23 |
| FGD Absorber Recirculation Pump | Limestone / gypsum slurry with chlorides | 50–65 °C | 1–4 bar | Slurry cartridge, external springs (catalogue ref. HS860) | Sintered SiC vs sintered SiC / FKM or EPDM | API Plan 32 (clean water flush) or Plan 62 quench, per seal design |
| FGD Limestone Slurry Feed Pump | Limestone slurry | Ambient–40 °C | 2–5 bar | Slurry cartridge, external springs (catalogue ref. HS860) | Sintered SiC vs sintered SiC / EPDM | API Plan 32 or Plan 62, per seal design |
| FGD Gypsum Bleed / Hydrocyclone Feed Pump | Gypsum slurry | 50–65 °C | 2–5 bar | Double cartridge, back-to-back (pressurised) | SiC vs SiC (both seals) / FKM | API Plan 53A (barrier ≥ 1.4 bar above seal chamber) or Plan 54 |
| Bottom Ash / Fly Ash Slurry Pump | Ash slurry | 30–60 °C | Up to 8 bar per stage; for pumps in series, rate the seal for the highest stage | Slurry cartridge, external springs (catalogue ref. HS860) | Tungsten carbide (Ni binder) vs tungsten carbide, or SiC vs SiC / FKM | API Plan 32 (regulated clean water flush, ≈ 1 bar above seal chamber) |
| HFO / LDO Pump (boiler start-up & support) | Heavy fuel oil (heated) or light diesel oil | HFO 90–130 °C; LDO ambient | 10–30 bar | Balanced multi-spring cartridge | SiC vs carbon / FKM; metal bellows with flexible graphite secondary seals where the steam quench exceeds the FKM temperature limit | API Plan 02 (screw pumps: seal at suction pressure) or Plan 11 (centrifugal pumps); add Plan 62 steam quench on HFO to prevent coking |
Reviewed by Gipfel Engineering’s technical team.
Technical Information Disclaimer
The information on this page, including process descriptions, flow diagrams, operating ranges, seal arrangements, materials and piping plans, is general technical guidance for information only. Values shown are typical industry ranges, not guaranteed ratings or specifications of any Gipfel Engineering product. Each application differs. Seal selection, material compatibility, installation and operation must be verified by qualified personnel against the specific equipment data sheet, process conditions, applicable codes and the pump manufacturer’s instructions. A binding recommendation is given only in a written quotation or technical offer from Gipfel Engineering.
References to standards (such as API 682, ISO 21049, ISO 3069, FDA 21 CFR 177.2600 and NACE MR0175 / ISO 15156) describe common industry practice. They do not mean that any product is certified, qualified or approved to that standard unless this is confirmed in writing for a specific order. Third-party company and product names, including “equivalent to” references, are used for identification only and remain the trademarks of their owners. No affiliation, endorsement or OEM approval is implied.
Compliance with safety, hazardous-area, environmental and statutory requirements at the user’s site remains the responsibility of the plant owner or operator. To the extent permitted by law, Gipfel Engineering accepts no liability for loss or damage arising from reliance on this general information without a confirmed written recommendation. Content may change without notice.