Sugar Refinery
Process Overview
Sugar Refinery — Process Overview
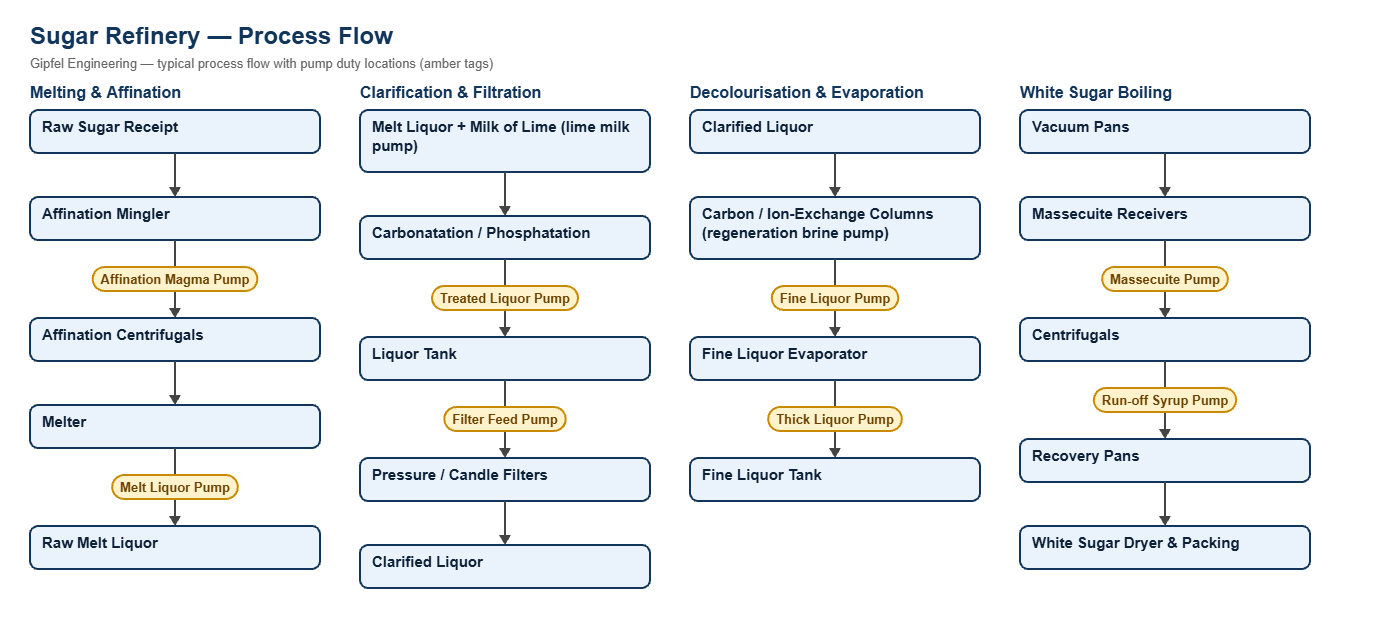
A sugar refinery, standalone or attached to a cane sugar mill, converts raw sugar into refined white sugar. Raw sugar is affined and melted, the melt liquor is clarified by carbonatation or phosphatation and filtered, decolourised with activated carbon or ion-exchange resins, concentrated in evaporators, and boiled to white sugar in vacuum pans before curing, drying and packing. Sticky high-Brix liquors, crystal magmas, lime and calcium carbonate slurries and regeneration brines set the sealing requirements.
Process Stages & Sealing Focus:
- Affination & melting: crystal magma on positive-displacement pumps needs hard face pairs and a clean barrier.
- Clarification & filtration: lime and carbonate precipitates are abrasive; filter feed pumps see cyclic pressure.
- Decolourisation: ion-exchange regeneration uses salt brine and caustic.
- Evaporation & boiling: thick liquor under vacuum and white massecuite crystallise at the atmospheric side.
- Recovery & sweetwater: run-off syrups and dilute sugar water.
Related: Cane Sugar Mill · Food & Beverage.
Which mechanical seals are used in a sugar refinery?
Refinery liquor pumps typically use single balanced cartridge seals with a hot-water quench (Plan 62) to dissolve sugar weepage. Lime and carbonate slurries use slurry cartridge seals (e.g. Gipfel HS860), while thick liquor under vacuum and massecuite or magma pumps use dual cartridge seals with a clean water barrier (Plan 53A or 54).
Root-Cause Failure Analysis — Field Example
Symptom: Carbonatation liquor pump seal leaks within weeks; faces grooved and springs packed.
  ├── Diagnostic Evidence Required:
  │     ├── Are the faces scored by calcium carbonate particles?
  │     ├── Is carbonate scale building up behind the dynamic O-ring?
  │     ├── Is there no flush or quench?
  └── Engineered Solution:
        ├── Fit a slurry cartridge with tungsten carbide vs SiC faces and springs out of the product.
        ├── Add a clean water flush (Plan 32) or continuous quench (Plan 62).
        ├── Flush the seal chamber before shutdowns.
Frequently Asked Questions
Why do refinery liquor pump seals stick after a stop?
Sugar liquor that weeps across the faces dries into crystals on the atmospheric side. A continuous hot-water quench (Plan 62) dissolves it before it can hold the faces.
Which seals suit massecuite and magma pumps?
These are usually positive-displacement pumps handling crystals in syrup. Heavy-duty dual seals with tungsten carbide face pairs and a clean water barrier (Plan 54) resist crystal crushing and crusting.
Request a Seal Selection
Send your pump make and model, fluid, Brix, temperature, pressure, shaft size and speed to info@gipfelengg.com or use our enquiry form. Gipfel Engineering (ISO 9001:2015, NSIC-registered MSME, Mumbai) designs and manufactures mechanical seals, seal support systems and process pumps.
Equipment solutions: Overhung Pumps · Positive Displacement Pumps · Slurry Pumps.
Sugar Refinery Pump Duty & Mechanical Seal Selection Matrix
Typical values for selection guidance only. Final selection is made against the refinery duty sheet; food-contact elastomer grades on request.
| Pump duty | Fluid | Typical temp. | Typical pressure (bar) | Seal arrangement | Faces / elastomer | API piping plan |
|---|---|---|---|---|---|---|
| Melt Liquor | Raw melt liquor, high Brix | 75–85°C | 3–5 | Single balanced cartridge | SiC vs SiC / EPDM | API Plan 11 + Plan 62 hot-water quench |
| Affination Magma (PD pump) | Magma: sugar crystals in syrup | 50–65°C | 4–8 | Heavy-duty dual cartridge | Tungsten carbide vs tungsten carbide / Aflas | API Plan 54 (clean water barrier) |
| Milk of Lime | Ca(OH)2 slurry, abrasive | Ambient–60°C | 3.0–4.5 | Slurry cartridge, springs out of the product (catalogue ref. HS860) | Tungsten carbide vs SiC / EPDM | API Plan 32 or Plan 62 quench |
| Carbonatation / Phosphatation Liquor | Liquor with lime or calcium carbonate precipitate | 75–85°C | 3.5–5.5 | Slurry cartridge (catalogue ref. HS860) | Tungsten carbide vs SiC / EPDM | API Plan 32 or Plan 62 quench |
| Pressure / Candle Filter Feed | Treated liquor with filter cake; cyclic pressure | 75–85°C | 2–6 (cyclic) | Dual pressure-balanced cartridge | Tungsten carbide vs SiC / EPDM | API Plan 53A (barrier ≥ 1.4 bar above the maximum cycle pressure) |
| Clarified / Fine Liquor | Filtered, decolourised liquor | 75–85°C | 3–5 | Single balanced cartridge | SiC vs SiC / EPDM | API Plan 11 + Plan 62 quench |
| Ion-Exchange Regeneration Brine | Salt brine with caustic | Ambient–60°C | 3.0–4.5 | Single chemical-duty cartridge, super duplex or alloy wetted parts | Sintered SiC vs sintered SiC (not reaction-bonded: caustic attacks free silicon) / EPDM | API Plan 11 + Plan 62 quench |
| Evaporator Thick Liquor (vacuum) | Thick fine liquor | 70–85°C | −0.8 to +4 | Dual pressurised cartridge | SiC vs SiC / EPDM or Aflas | API Plan 53A (barrier ≥ 1.4 bar above seal-chamber pressure) |
| White Massecuite (PD pump) | Massecuite: white sugar crystals in syrup | 60–75°C | 6–10 | Heavy-duty dual cartridge | Tungsten carbide vs tungsten carbide / Aflas | API Plan 54 (clean water barrier) |
| Run-off / Recovery Syrup | High-Brix syrup | 65–80°C | 3–5 | Wave spring heavy-viscosity cartridge | SiC vs SiC / EPDM | API Plan 11 + Plan 62 quench |
| Sweetwater / Condensate | Dilute sugar water, condensate | 60–90°C | 2.5–4.0 | Single balanced cartridge | Carbon vs SiC / EPDM | API Plan 11 |
Reviewed by Gipfel Engineering’s technical team.
Technical Information Disclaimer
The information on this page, including process descriptions, flow diagrams, operating ranges, seal arrangements, materials and piping plans, is general technical guidance for information only. Values shown are typical industry ranges, not guaranteed ratings or specifications of any Gipfel Engineering product. Each application differs. Seal selection, material compatibility, installation and operation must be verified by qualified personnel against the specific equipment data sheet, process conditions, applicable codes and the pump manufacturer’s instructions. A binding recommendation is given only in a written quotation or technical offer from Gipfel Engineering.
References to standards (such as API 682, ISO 21049, ISO 3069, FDA 21 CFR 177.2600 and NACE MR0175 / ISO 15156) describe common industry practice. They do not mean that any product is certified, qualified or approved to that standard unless this is confirmed in writing for a specific order. Third-party company and product names, including “equivalent to” references, are used for identification only and remain the trademarks of their owners. No affiliation, endorsement or OEM approval is implied.
Compliance with safety, hazardous-area, environmental and statutory requirements at the user’s site remains the responsibility of the plant owner or operator. To the extent permitted by law, Gipfel Engineering accepts no liability for loss or damage arising from reliance on this general information without a confirmed written recommendation. Content may change without notice.