Sulphuric Acid Plant
Process Overview
Sulphuric Acid Plant — Process Overview
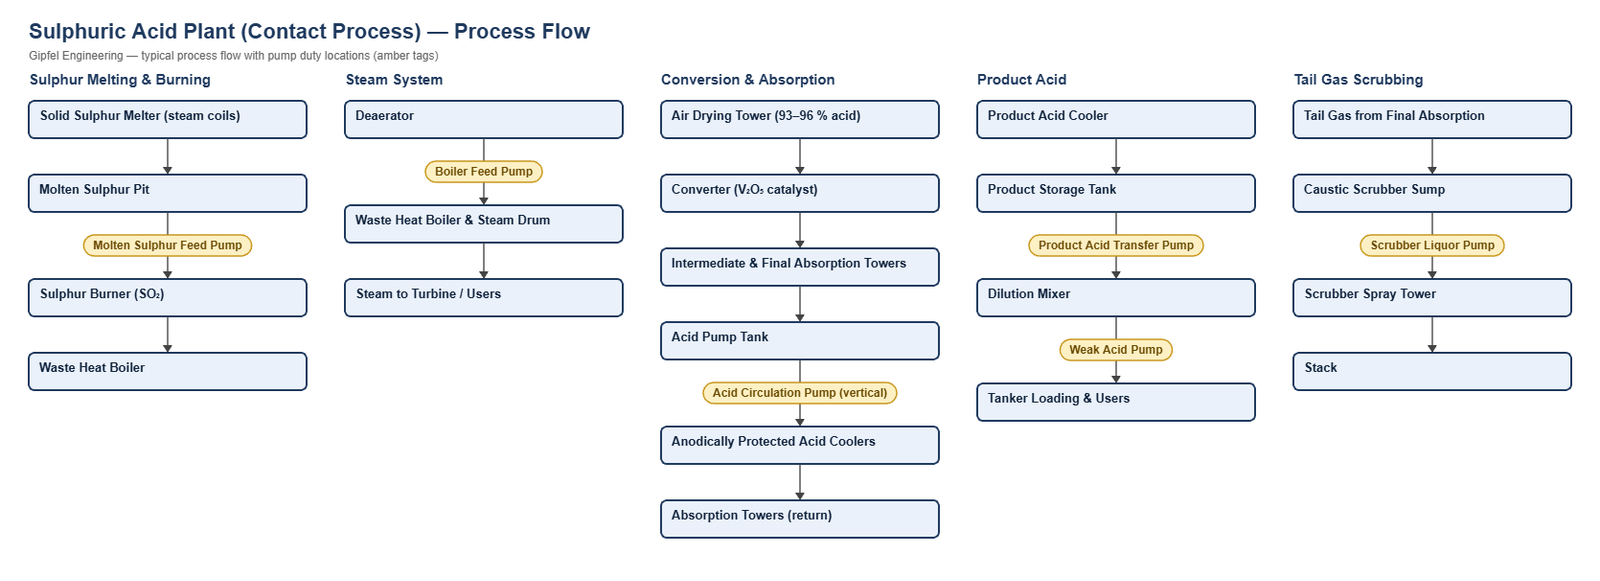
In a sulphur-burning contact plant, molten sulphur is burned in dried air to form SO₂, converted to SO₃ over vanadium pentoxide catalyst and absorbed in circulating 98–98.5 % sulphuric acid. A drying tower using 93–96 % acid dries the process air, a waste heat boiler raises steam from the combustion heat, and product acid is cooled, diluted where required and loaded out.
For acid and caustic duties in salt electrolysis see Chlor-Alkali; for phosphoric acid production see Fertiliser.
Key Sealing Challenges
- Concentrated acid: hot 93–98.5 % acid oxidises carbon and attacks most elastomers. Sintered SiC faces with FFKM or PTFE secondary seals and high-alloy metal parts are used.
- No water near the seal: a water quench or water-based flush dilutes the acid at the faces, releasing heat and making it far more corrosive.
- Molten sulphur: it solidifies on cooling, so the seal chamber is steam-jacketed and the atmospheric side is steam-quenched.
- Waste heat boiler: hot feedwater duties follow power-plant practice with API Plan 23.
What mechanical seal is used for concentrated sulphuric acid pumps?
Horizontal pumps on 93–98.5 % sulphuric acid typically use a balanced cartridge seal with sintered silicon carbide vs. sintered silicon carbide faces, FFKM or PTFE secondary seals and Alloy 20 or Hastelloy C-276 metal parts on an API Plan 11 flush. Carbon faces are avoided in hot concentrated acid, and a water quench must not be used. Main circulation pumps are often vertical cantilever designs sealed above the liquid level according to the pump OEM.
Root-Cause Failure Analysis — Field Example
Symptom: Product acid pump seal fails within weeks; metal parts pitted, faces heavily etched.
  ├── Incorrect Response: "Change to tungsten carbide faces."
  ├── Diagnostic Evidence Required:
  │     ├── Was a water quench or water flush connected to the gland? Dilution at the faces creates hot, highly corrosive weak acid.
  │     ├── Check acid concentration and temperature at the pump against the seal material limits.
  │     └── Identify face grade: reaction-bonded SiC or cobalt-bound tungsten carbide are attacked; carbon oxidises in hot strong acid.
  └── Engineered Solution:
        ├── Remove the water quench; use API Plan 11 from pump discharge.
        ├── Sintered SiC vs sintered SiC faces with FFKM or PTFE secondary seals.
        └── Alloy 20 or Hastelloy C-276 metal parts selected for the actual acid concentration and temperature.
Frequently Asked Questions
Why is a water quench not used on concentrated sulphuric acid seals?
Concentrated sulphuric acid is less corrosive to many alloys than dilute acid. Water at the seal faces dilutes the leakage, releases heat of dilution and creates exactly the weak, hot acid that attacks metal parts and faces.
Which seal suits molten sulphur pumps?
A metal bellows seal with flexible graphite secondary seals and SiC vs carbon faces, mounted in a steam-jacketed seal chamber (API Plan 02) with an API Plan 62 steam quench, keeps the sulphur molten at the faces and on the atmospheric side.
Related: Chlor-Alkali · Fertiliser · General Chemical Plants · Coal-Fired Thermal Power.
Request a Seal Selection
Send your pump make and model, fluid, concentration, temperature, pressure, shaft size and speed to info@gipfelengg.com or use our enquiry form. Gipfel Engineering (ISO 9001:2015, NSIC-registered MSME, Mumbai) designs and manufactures mechanical seals, seal support systems and process pumps.
Equipment solutions: Overhung Pumps · Vertical & Sump Pumps · Agitators.
Pump Duty & Mechanical Seal Selection Matrix
Typical values for selection guidance only. Final selection is made against the customer duty sheet.
| Pump duty | Fluid | Typical temp. | Typical pressure (bar) | Seal arrangement | Faces / elastomer | API piping plan |
|---|---|---|---|---|---|---|
| Molten Sulphur Feed Pump (horizontal) | Molten sulphur | 135–150 °C (sulphur solidifies near 115–120 °C; viscosity rises sharply above about 160 °C) | 5–15 bar | Metal bellows seal | SiC vs carbon / flexible graphite secondary seals | API Plan 02 (steam-jacketed seal chamber) + Plan 62 steam quench |
| Acid Circulation Pump — Drying & Absorption Towers | 93–98.5 % H₂SO₄ | 70–120 °C | 2–5 bar | Usually vertical cantilever pumps with the shaft seal above the liquid level, per pump OEM. Seal selection on request | — | No water quench on concentrated acid |
| Product Acid Transfer / Loading Pump | 98 % H₂SO₄ (cooled) | 30–50 °C | 3–6 bar | Balanced multi-spring cartridge with Alloy 20 or Hastelloy C-276 metal parts | Sintered SiC vs sintered SiC / FFKM or PTFE | API Plan 11. No water quench: dilution releases heat and makes the acid far more corrosive |
| Weak Acid / Dilution Pump | 20–70 % H₂SO₄ | Ambient–60 °C | 2–5 bar | Balanced multi-spring cartridge with Alloy 20 or Hastelloy C-276 metal parts | Sintered SiC vs sintered SiC / FKM or FFKM | API Plan 11 |
| Waste Heat Boiler Feed Pump | Deaerated feedwater | 105–150 °C | Seal sees seal-chamber (suction / balance-line) pressure, not discharge — confirm per pump | High-pressure balanced cartridge, stationary springs (catalogue ref. HP760) | Reaction-bonded SiC vs carbon / EPDM (peroxide-cured) or FEPM (Aflas) | API Plan 23 |
| Acid Cooler Cooling Water Pump | Cooling water | 30–40 °C | 2–5 bar | Balanced multi-spring cartridge | SiC vs SiC / EPDM | API Plan 11 (clarified water) or Plan 32 (silt-laden water) |
| Tail Gas Scrubber Liquor Pump | Caustic / sodium sulphite solution | 30–50 °C | 2–4 bar | Balanced multi-spring cartridge | Sintered SiC vs sintered SiC (not reaction-bonded: free silicon is attacked by caustic) / EPDM | API Plan 11 + Plan 62 water quench against crystallisation |
Reviewed by Gipfel Engineering’s technical team.
Technical Information Disclaimer
The information on this page, including process descriptions, flow diagrams, operating ranges, seal arrangements, materials and piping plans, is general technical guidance for information only. Values shown are typical industry ranges, not guaranteed ratings or specifications of any Gipfel Engineering product. Each application differs. Seal selection, material compatibility, installation and operation must be verified by qualified personnel against the specific equipment data sheet, process conditions, applicable codes and the pump manufacturer’s instructions. A binding recommendation is given only in a written quotation or technical offer from Gipfel Engineering.
References to standards (such as API 682, ISO 21049, ISO 3069, FDA 21 CFR 177.2600 and NACE MR0175 / ISO 15156) describe common industry practice. They do not mean that any product is certified, qualified or approved to that standard unless this is confirmed in writing for a specific order. Third-party company and product names, including “equivalent to” references, are used for identification only and remain the trademarks of their owners. No affiliation, endorsement or OEM approval is implied.
Compliance with safety, hazardous-area, environmental and statutory requirements at the user’s site remains the responsibility of the plant owner or operator. To the extent permitted by law, Gipfel Engineering accepts no liability for loss or damage arising from reliance on this general information without a confirmed written recommendation. Content may change without notice.