Refinery Treating & Light Ends
Process Overview
Refinery Treating & Light Ends — Process Overview
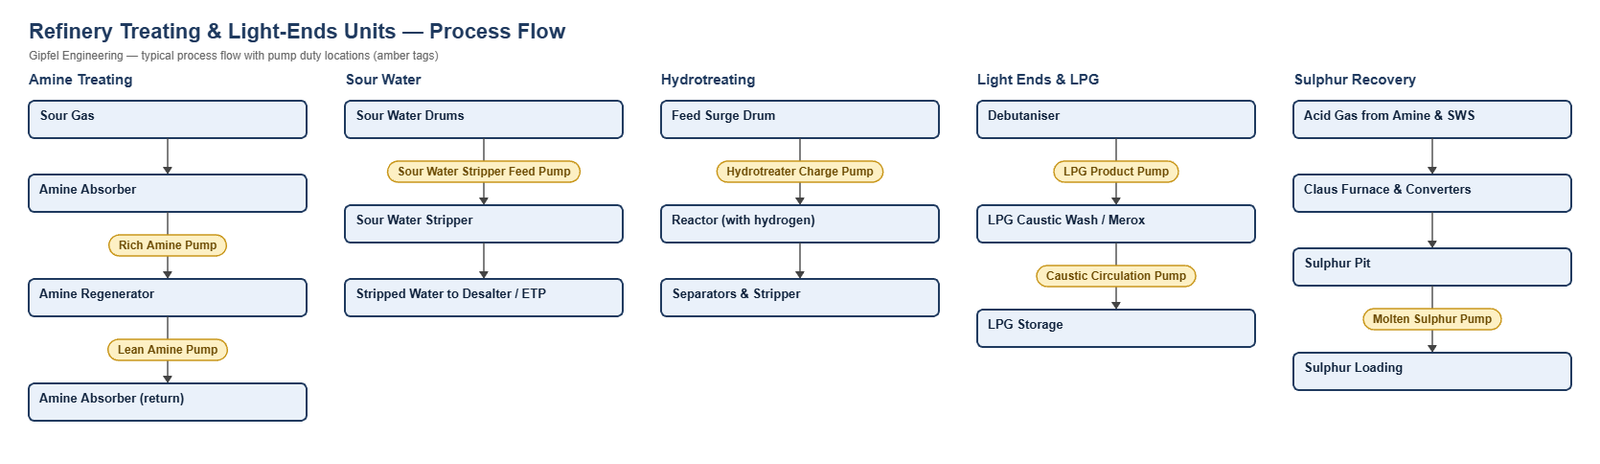
Treating units remove sulphur and other contaminants from refinery streams and recover saleable light ends. Amine units absorb H₂S from fuel gas and hydrogen recycle; sour water strippers remove H₂S and ammonia from process condensate; hydrotreaters remove sulphur from naphtha and diesel over catalyst with hydrogen; debutanisers and caustic or Merox treaters produce sweet LPG; and the sulphur recovery unit (Claus) converts acid gas into molten sulphur.
For crude, vacuum, FCC and coker units see Refinery Crude, Vacuum & Conversion Units.
Key Sealing Challenges
- Toxic fluids: H₂S-laden amine and sour water use Arrangement 2 tandem seals with a Plan 52 buffer vented to flare.
- Elastomer compatibility: amines and ammonia attack FKM, and hydrocarbons attack EPDM, so FFKM is the safe choice where both are present.
- Volatile light ends: LPG flashes at the faces unless seal-chamber pressure is kept above vapour pressure.
- Crystallising and solidifying fluids: caustic needs a water quench; molten sulphur needs a steam-jacketed chamber and steam quench.
What mechanical seal is used on refinery amine pumps?
Rich amine pumps typically use a tandem double cartridge seal (Arrangement 2) with silicon carbide vs. silicon carbide faces and FFKM elastomers on API Plan 11 + Plan 52, with the buffer vented to flare. Amine attacks FKM, and the hard face pair resists the iron sulphide particles that circulate in amine systems.
Root-Cause Failure Analysis — Field Example
Symptom: Rich amine pump seal faces wear in a few months; black deposits on the faces and in the buffer reservoir.
  ├── Incorrect Response: "Increase flush flow."
  ├── Diagnostic Evidence Required:
  │     ├── Analyse the deposits: iron sulphide from corrosion in the amine circuit?
  │     ├── Check face materials: is a carbon face wearing against the particles?
  │     └── Check amine filtration and degradation (heat-stable salts).
  └── Engineered Solution:
        ├── SiC vs SiC hard face pair on the inboard seal.
        ├── Restore amine filtration upstream of the pump.
        └── Tandem seal with Plan 52 buffer vented to flare; monitor buffer pressure for inner-seal leakage.
Frequently Asked Questions
Why is FFKM used on sour water pumps?
Sour water contains ammonia, which attacks FKM, and oil, which attacks EPDM. FFKM resists both, along with H₂S and phenols.
How is vapour pressure margin maintained on LPG pumps?
The seal chamber is kept above the fluid’s vapour pressure, typically with an API Plan 11 flush from discharge or a Plan 13 return to suction where the chamber pressure needs lowering. Without margin, LPG flashes between the faces and the seal runs dry.
Related: Refinery Crude, Vacuum & Conversion Units · Sulphuric Acid · Upstream Oil & Gas · Pipelines, Terminals & LPG.
Request a Seal Selection
Send your pump make and model, fluid, temperature, pressure, shaft size and speed to info@gipfelengg.com or use our enquiry form. Gipfel Engineering (ISO 9001:2015, NSIC-registered MSME, Mumbai) designs and manufactures mechanical seals, seal support systems and process pumps.
Equipment solutions: Overhung Pumps · Vertical & Sump Pumps · Compressors & Bearing Chambers.
Pump Duty & Mechanical Seal Selection Matrix
Typical values for selection guidance only. Final selection is made against the customer duty sheet.
| Pump duty | Fluid | Typical temp. | Typical pressure (bar) | Seal arrangement | Faces / elastomer | API piping plan |
|---|---|---|---|---|---|---|
| Rich Amine Pump | Rich MDEA / DEA loaded with H₂S and CO₂ | 50–80 °C | Seal-chamber pressure — confirm per pump | Tandem double cartridge (Arrangement 2) | SiC vs SiC / FFKM (amines attack FKM) | API Plan 11 + Plan 52 (buffer vented to flare) |
| Lean Amine Pump | Lean amine with hydrocarbon traces | 40–60 °C | Discharge to absorber pressure; seal sees suction pressure — confirm per pump | Balanced multi-spring cartridge | SiC vs SiC / FFKM | API Plan 11 |
| Sour Water Stripper Feed Pump | Sour water with H₂S, ammonia, phenols and oil | 40–90 °C | 3–8 bar | Tandem double cartridge (Arrangement 2) | SiC vs SiC / FFKM (ammonia and hydrocarbons rule out FKM and EPDM respectively) | API Plan 11 + Plan 52 (buffer vented to flare) |
| Hydrotreater Charge Pump | Naphtha or diesel feed | 60–150 °C | Discharge 60–150 bar; seal sees seal-chamber pressure — confirm per pump | API 682 cartridge seal (Arrangement 1) | SiC vs carbon / FKM, or FFKM above the FKM temperature limit | API Plan 11, or Plan 23 for hot feed |
| Debutaniser Bottoms / LPG Product Pump | LPG, high vapour pressure | 40–80 °C | Keep seal-chamber pressure margin above vapour pressure | Tandem double cartridge (Arrangement 2) | Carbon vs SiC / FKM | API Plan 11 + Plan 52 (buffer vapour to flare or recovery) |
| Caustic Wash / Merox Circulation Pump | 5–20 % caustic with mercaptides and hydrocarbons | Ambient–50 °C | 3–8 bar | Balanced multi-spring cartridge | Sintered SiC vs sintered SiC / FFKM | API Plan 11 + Plan 62 water quench against caustic crystallisation |
| Molten Sulphur Pump (SRU) | Molten sulphur | 135–150 °C | 3–10 bar | Metal bellows seal | SiC vs carbon / flexible graphite | API Plan 02 (steam-jacketed seal chamber) + Plan 62 steam quench |
Reviewed by Gipfel Engineering’s technical team.
Technical Information Disclaimer
The information on this page, including process descriptions, flow diagrams, operating ranges, seal arrangements, materials and piping plans, is general technical guidance for information only. Values shown are typical industry ranges, not guaranteed ratings or specifications of any Gipfel Engineering product. Each application differs. Seal selection, material compatibility, installation and operation must be verified by qualified personnel against the specific equipment data sheet, process conditions, applicable codes and the pump manufacturer’s instructions. A binding recommendation is given only in a written quotation or technical offer from Gipfel Engineering.
References to standards (such as API 682, ISO 21049, ISO 3069, FDA 21 CFR 177.2600 and NACE MR0175 / ISO 15156) describe common industry practice. They do not mean that any product is certified, qualified or approved to that standard unless this is confirmed in writing for a specific order. Third-party company and product names, including “equivalent to” references, are used for identification only and remain the trademarks of their owners. No affiliation, endorsement or OEM approval is implied.
Compliance with safety, hazardous-area, environmental and statutory requirements at the user’s site remains the responsibility of the plant owner or operator. To the extent permitted by law, Gipfel Engineering accepts no liability for loss or damage arising from reliance on this general information without a confirmed written recommendation. Content may change without notice.